Flexible Expandable Roller Conveyor from China Factory - Top Suppliers for Logistics & Warehousing Solutions
Advantages
1. Flexible Adaptability
Modular splicing design allows for convenient installation and disassembly. Length and conveying path can be adjusted as needed, maximizing space utilization and adapting to various scenarios for quick switching.
2. Smooth Conveying
The rollers utilize precision bearings for flexible rotation, ensuring smooth and uninterrupted material conveying and effectively reducing material damage.
3. Durable and Reliable
The rollers are made of high-quality stainless steel/carbon steel with powder coating, offering corrosion and wear resistance. The frame is constructed of high-strength aluminum alloy, ensuring lightweight construction and stable load-bearing capacity.
4. Easy Maintenance
Simple structure and standardized key components facilitate convenient daily maintenance. Modular additions and removals are supported as needed, resulting in low expansion costs in the future.
Product Description
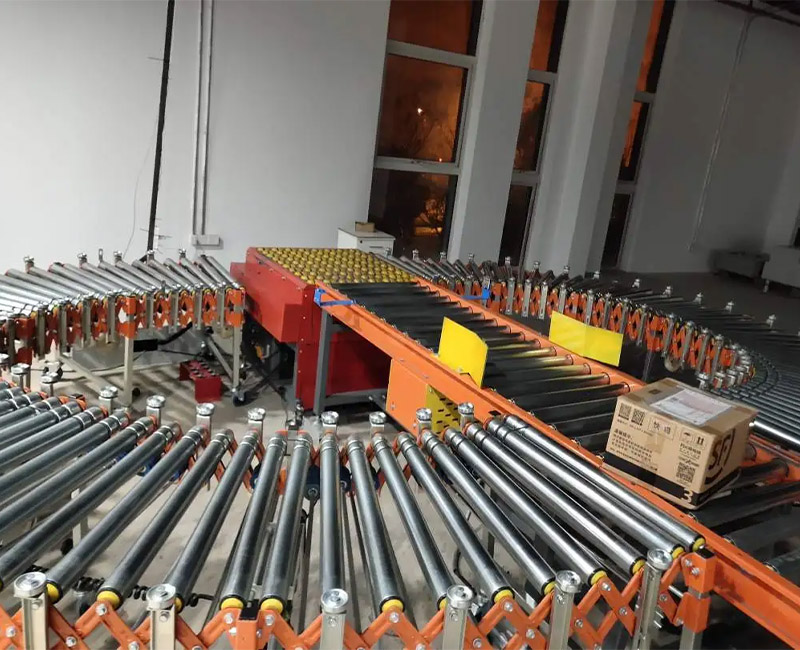
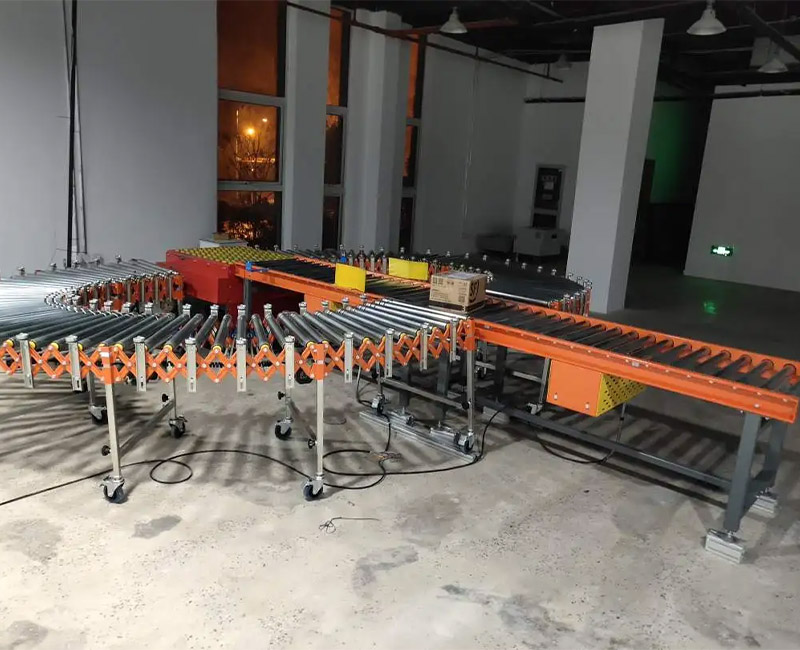
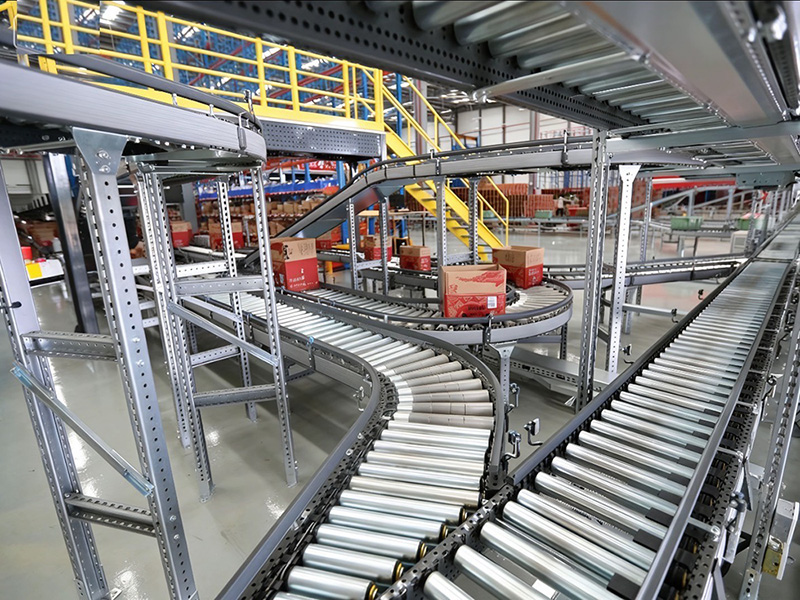
Flexible roller conveyors, with their modular and flexible design at their core, are suitable for the continuous conveying of various boxed, bagged, and palletized materials. They can be quickly assembled and disassembled to achieve conveying under various working conditions, including turning, telescopic, and incline operations. Widely used in warehousing and sorting, e-commerce logistics, electronics manufacturing, food and pharmaceutical industries, they can precisely connect with upstream and downstream conveying equipment, enhancing the flexibility and adaptability of production lines.
Product Specifications
| Parameter | Specification Parameters |
| Speed | Customizable |
| Load | Single roller load: 50-500kg; Line load: 100-500kg/m |
| Roller Diameter | 50mm, 60mm, 76mm, 89mm, 108mm, 150mm |
| Material | Stainless Steel 304/Galvanized |
| Frame Material | Aluminum profile/Carbon steel spray-painted/Stainless Steel (Customizable), height customizable |
| Drive Power | Variable frequency |
| Ambient Temperature | -10℃~80℃ |
| Wall Thickness | 1.0-3.0mm (Selected according to load requirements) |
| Certification | CE/ISO9001 |
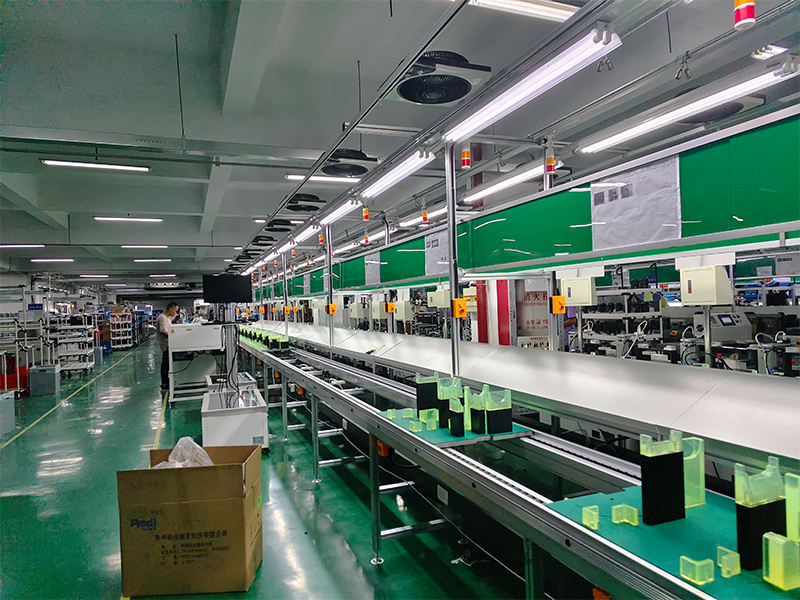
Successful Case
Frequently Asked Questions (FAQ)
What industries are flexible roller conveyors most suitable for?
They are widely utilized across warehousing logistics, e-commerce distribution centers, parcel sorting, food and beverage processing, pharmaceuticals, and manufacturing assembly lines requiring flexible routing.
Can the dimensions and loading capacity be customized?
Yes. The conveyor length, frame height, roller diameter, wall thickness, and overall loading capacity can be engineered according to your specific facility layouts and payload requirements.
What materials are available for the roller construction?
Rollers are primarily manufactured using high-grade Stainless Steel 304 or Galvanized Carbon Steel with optional powder coating to withstand heavy friction and resist corrosion.
How does the modular design benefit maintenance and scalability?
The modular setup allows individual components or sections to be rapidly replaced or added without extensive line downtime, drastically lowering routine maintenance costs and simplifying future expansions.
What quality certifications do these conveyor systems comply with?
All conveyor units comply with international industrial safety and management standards, holding certifications including CE and ISO9001.